Laboratory vs on-site immunity testing
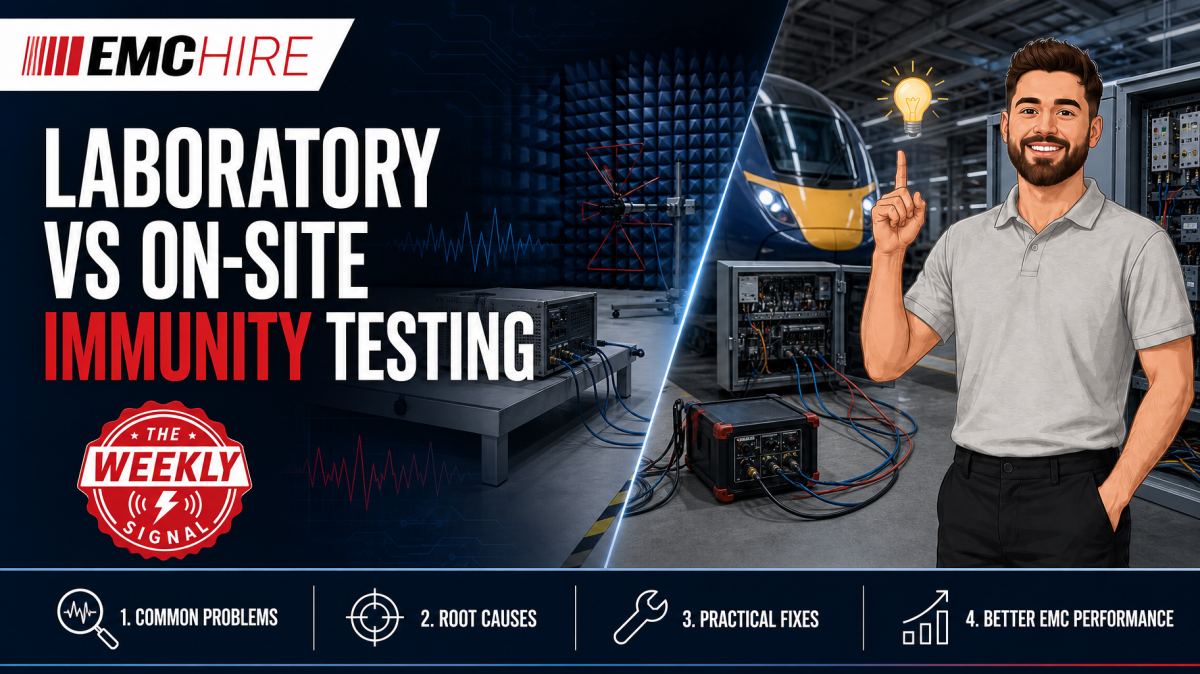
A representative laboratory test is better than a convenient site test, but a representative site test can be far more useful than laboratory testing a system stripped of its real cables, loads and installation bonds.
The decision is not simply about whether the equipment under test can fit through the laboratory door. Defence, rail and industrial teams must consider coupling paths, RF environment, installation state, safety controls, equipment logistics and the strength of the resulting compliance evidence. On-site immunity testing can preserve system context, but that advantage disappears if the field setup cannot produce controlled, repeatable and adequately documented stress levels.
What changes when immunity testing leaves the laboratory?
A laboratory is designed to control variables. Cable routing, ground planes, antenna distance, coupling devices, ambient conditions and EUT operating modes can be defined before testing begins. The same arrangement can then be reconstructed after a design change. That repeatability is particularly valuable when diagnosing intermittent resets, communication errors or analogue measurement drift.
At site, the installed system becomes part of the test arrangement. Cabinet bonding, long cable routes, building steelwork, trackside infrastructure, remote sensors, protective earth networks and connected loads can all alter the disturbance path. This is often the reason for testing in situ. It is also the source of additional measurement uncertainty and test risk.
Immunity is not one test. IEC 61000-4-x documents describe basic test methods for phenomena such as electrostatic discharge, radiated RF fields, electrical fast transient or burst, surge, conducted RF and power-frequency magnetic fields. The applicable product, product-family, contractual or military standard determines which methods apply, the ports to be tested, stress levels, performance criteria and configuration. The current active editions and project-specific test plan must be checked rather than treating a generic immunity method as a universal product requirement.
Laboratory control improves diagnostic resolution
Controlled testing makes cause and effect easier to separate. For radiated RF immunity, a characterised field arrangement allows the engineering team to correlate an EUT response with frequency, polarisation, modulation, field strength and antenna position. Moving an uncharacterised antenna around an equipment room may expose a weakness, but it does not automatically demonstrate that the required field was applied uniformly to the relevant faces of the EUT.
Conducted RF immunity requires the coupling method specified by the applicable procedure. A coupling and decoupling network, or CDN, may be used under IEC 61000-4-6 where suitable for the port and cable. Current-injection methods, including appropriately selected BCI probes, arise in applicable automotive, aerospace, military and other product-specific procedures. They are not interchangeable merely because both inject RF onto a cable.
Laboratory access also makes debugging quicker. Current probes, voltage probes and monitoring equipment can be repositioned without repeatedly stopping a live site process. Filters, bonding changes and cable treatments can be assessed under a stable stimulus. If the disturbance arrangement changes between each modification, an apparent improvement may simply be a change in coupling efficiency.
Installed context can dominate the response
Some systems cannot be represented adequately on a bench. A large variable-speed drive may depend on its production motor, screened motor cable, cabinet gland arrangement and plant earth network. A rail subsystem may interact with vehicle wiring, chassis bonds and remote interfaces. Defence equipment can have cable assemblies and platform installations that are difficult to reproduce without the actual installation.
In these cases, on-site immunity testing can reveal susceptibility mechanisms hidden by an abbreviated laboratory configuration. It can also expose interfaces that were omitted from subsystem testing. That does not make every site result suitable as formal compliance evidence. The method, instrumentation, calibration status, limitations and deviations need to be recorded, and the acceptance route agreed with the responsible parties.
Where calibration affects the measurement, EMC Hire uses test equipment with calibration traceable through an appropriate ISO/IEC 17025 accredited calibration provider. Suitable traceability supports repeatability, confidence in recorded data and comparison between development and formal testing. The accreditation relates to the calibration laboratory or activity, not to the physical instrument itself. Further guidance on the role of accredited calibration is available from UKAS.
Choosing between lab hire and a field setup
Laboratory testing is generally preferable when the EUT can be transported safely, its installation can be reproduced and the required method depends on tightly controlled geometry. Access to a suitable facility reduces ambient variables and provides a more defensible basis for repeat measurements.
A lab hire arrangement can suit development teams that already understand the method and need temporary access to space, coupling equipment or monitoring resources. Engineering support remains useful when the intended configuration falls outside a straightforward tabletop product. A poorly chosen ground plane or unrealistic cable layout can produce very repeatable results for the wrong physical arrangement.
On-site work becomes the stronger option when moving the EUT would materially change it, when disassembly introduces greater project risk, or when the installation itself is part of the electromagnetic environment. Typical candidates include fixed machinery, large cabinets, production lines, installed rail equipment and integrated defence systems.
The choice should be made phenomenon by phenomenon. ESD testing might be practical at site while radiated RF immunity is constrained by access, field control or RF safety. Surge or burst testing may be possible on selected ports, but connection to operational plant can create safety and continuity risks. A hybrid programme often gives better engineering evidence: controlled subsystem testing in the laboratory, followed by targeted investigation of installation-dependent interfaces on site.
Site safety and operational constraints
Immunity generators can expose personnel and connected equipment to electrical, electromagnetic and operational hazards. Before arriving at site, the team should define exclusion zones, isolation arrangements, emergency stops, permit requirements, communication methods and responsibility for returning the plant to service. The site owner must also identify hazardous areas, safety-related functions and processes that cannot tolerate unintended interruption.
Radiated RF testing requires control of personnel exposure and unintended coupling into nearby systems. Surge testing can involve high voltages and significant source energy. ESD testing near flammable materials or explosive atmospheres may be unacceptable. Generic risk assessments copied from laboratory work are not enough. The assessment must reflect the actual plant and task, with reference to relevant HSE risk assessment guidance.
Typical scenario
Consider an industrial control cabinet integrated into a production machine with long sensor cables, a motor drive and network connections to adjacent plant. This is an illustrative example, not a customer case. The cabinet can technically be removed, but laboratory testing would replace the production motor, shorten cable runs and disconnect several interfaces. Those changes remove coupling paths that may govern the real susceptibility.
The engineering team first identifies the applicable product or product-family standard, contractual requirements and intended electromagnetic environment. Generic industrial immunity requirements may be relevant, but their scope must be verified. EMC Hire's information on generic immunity testing provides a starting point for discussing environments where no more specific product standard takes precedence.
A sensible programme might use laboratory testing for accessible control modules and targeted on-site immunity testing for the assembled installation. Conducted RF could be investigated on selected cable ports using the specified coupling method, while ESD is applied only at defined accessible points under controlled operating conditions. Radiated RF testing would proceed only if the required field, distance, monitoring and safety controls could be achieved credibly at the site.
The decisions are practical: which functions must be monitored, what constitutes degraded performance, whether automatic recovery is acceptable, and how surrounding plant will be protected. Testing the machine only in standby may miss susceptibility in high-current switching states. Conversely, forcing an unsafe operating mode simply to maximise activity is poor engineering.
Early investigation allows filtering, shielding, firmware recovery and bonding changes to be assessed before a formal programme. It can generate calibrated engineering data and improve confidence, but pre-compliance results do not automatically prove compliance. EMC Hire can support equipment selection, field setup, pre-compliance investigation, facility access and formal compliance testing where appropriate. For practical planning considerations, see EMC Hire's on-site testing services.
When to Hire EMC Equipment
Hiring is well suited to irregular immunity programmes. RF amplifiers, generators, directional couplers, power meters, field probes, CDNs, injection probes and transient generators must match the method, frequency range, power requirement, port type and intended test level. Buying a convenient unit before those parameters are settled can leave the team owning equipment that cannot support the next product programme.
Rental avoids unnecessary capital expenditure for a defined development window and removes much of the long-term burden of storage, servicing and calibration management. It also allows capability to scale during project peaks without building a permanent laboratory around short-lived demand.
Selection still requires engineering judgement. An RF amplifier must provide adequate output across the required range when cable loss, coupling-device insertion loss and levelling margin are included. A CDN must suit the port and conductor arrangement. A BCI probe must support the applicable injection method and usable frequency range. Hiring the wrong transducer wastes test time and can produce false confidence even when every instrument appears to be operating normally.
For teams considering CE or UKCA-related work, commercial EMC and self-certification testing support explains how engineering evidence can contribute to a technical file, Declaration of Conformity and risk-based conformity process. The manufacturer or responsible economic operator remains responsible for identifying the applicable legislation, standards, conformity assessment route and documentation. Testing alone does not complete every obligation.
Common EMC Testing Mistakes to Avoid
Treating the installation as an uncontrolled test jig
Unrecorded cable movement can change common-mode coupling enough to obscure the effect of a design modification. Photograph cable positions, record lengths and terminations, and identify every connected peripheral. Without that record, a later retest may not reproduce either the failure or the apparent fix.
Using the wrong coupling device
A CDN intended for conducted RF immunity is not a LISN. A LISN is used for conducted emissions measurements on relevant power ports. Likewise, selecting a BCI probe where the procedure requires a CDN changes the injection mechanism and calibration approach. The resulting stress may be poorly defined or incompatible with the specified method.
Ignoring performance monitoring
A machine that does not reset may still fail its stated performance criterion through corrupted data, control error or temporary loss of communication. Monitoring should capture the functions that matter, with synchronised records of frequency, test level, dwell and EUT response. Operator recollection is not an adequate evidence trail.
Assuming ambient RF is harmless
Site transmitters can mask low-level monitoring signals, affect field measurements or pre-condition the EUT before the intended stimulus is applied. A pre-test survey and suitable monitoring help distinguish the applied disturbance from the existing RF environment.
Mixing emissions and immunity conclusions
Passing immunity testing says nothing about disturbance emissions. Conducted emissions commonly involve a receiver and LISN on relevant power ports, while radiated emissions require suitable antennas and a defined measurement environment. Separate planning may be needed, as outlined in EMC Hire's guidance on generic emissions testing.
Leaving deviations out of the report
Installed systems often require departures from a preferred laboratory arrangement. Hiding those constraints weakens the report. State what differed, why it differed, how the effect was assessed and what limitation remains. A candid engineering record is more defensible than an overstated claim of conformity.
Frequently Asked Questions (FAQs)
Can on-site immunity testing be used for formal compliance?
Potentially, where the applicable requirements permit it and the method can be implemented with adequate control, calibration, safety and documentation. Contractual or sector requirements may call for testing by an appropriately accredited laboratory. Defence, rail and industrial teams should agree the evidence route before testing.
Is a laboratory always more repeatable?
Usually, but not automatically. A poorly documented laboratory setup can be less repeatable than a disciplined field setup. Laboratories offer better environmental control, while repeatability still depends on cable geometry, EUT state, coupling-device placement, calibration and monitoring.
When should radiated RF immunity remain in the laboratory?
Laboratory testing is generally preferable where field uniformity, antenna geometry, RF containment or personnel exposure cannot be controlled at site. Large installed systems may justify site work, but the achievable method and limitations need assessment before equipment is mobilised.
Can pre-compliance data support self-certification?
Calibrated, well-documented pre-compliance data can contribute to engineering assessment and the technical file where legally and technically appropriate. It does not guarantee compliance. The responsible manufacturer must confirm the applicable requirements and whether additional formal evidence is needed.
What records should be captured during field testing?
Record the EUT configuration, software, operating mode, cables, peripherals, bonds, test points, equipment identifiers, calibration status, applied parameters, performance criteria, observed responses, ambient conditions, deviations and photographs. Missing configuration data can make a technically sound test impossible to reproduce.
Planning a defensible immunity programme
The strongest programme is not necessarily all laboratory or all on site. It assigns each disturbance test to the environment where the EUT configuration is representative and the stimulus can be controlled. Check the latest active edition of every relevant standard, together with product-specific requirements, test levels, frequency ranges, configurations, methods, performance criteria and documentation obligations. Customer and contractual plans may add further constraints.
EMC Hire can help review the intended setup, identify suitable hire equipment, arrange lab hire, support on-site testing, provide pre-compliance engineering and discuss formal compliance testing where appropriate. To review a defence, rail or industrial immunity project, call +44 (0)1462 817111 or email sales@emchire.co.uk. The same discussion can cover equipment hire quotations and booking space at the EMC Hire test facility.
Disclaimer: Content is for informational purposes only and does not constitute formal engineering or regulatory advice. Always verify testing procedures against current official standards (e.g., ISO, MIL-STD, DEF STAN). EMC Hire Limited accepts no liability for outcomes resulting from the use of this information.