


Why ESD testing fails at the connector first
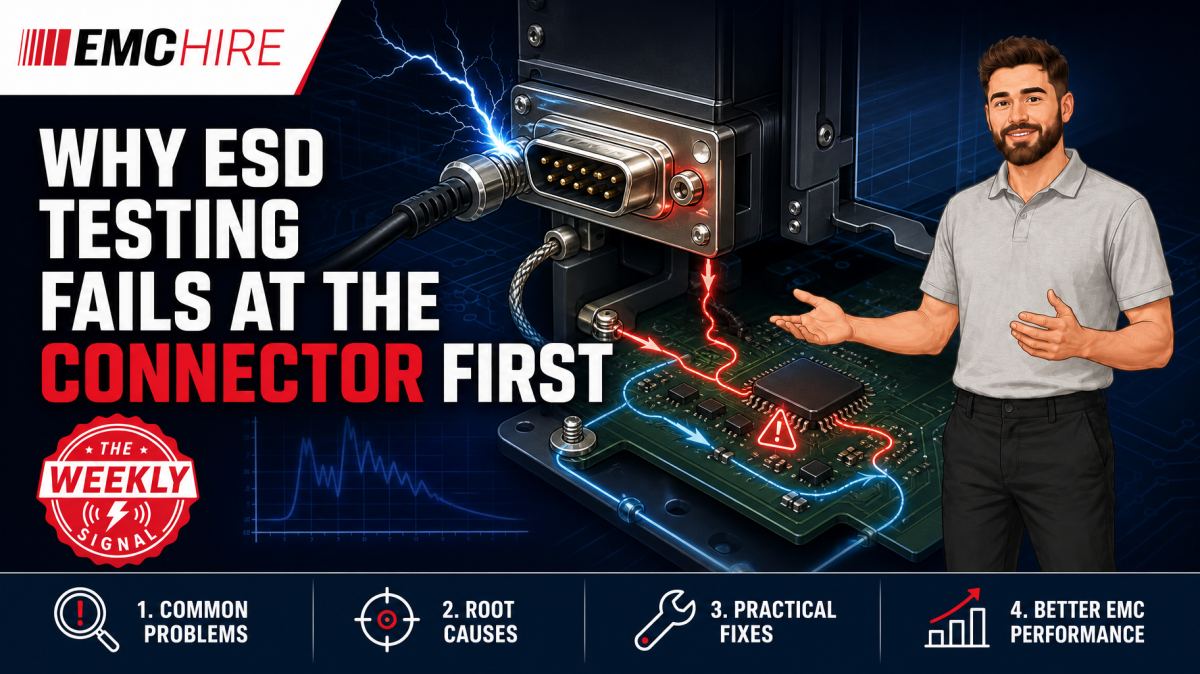
The connector is often blamed because that is where the discharge is applied. The actual failure may occur several centimetres away, after the connector has directed a fast current transient through the worst possible return path.
Why connectors attract ESD problems
Connectors combine several characteristics that make them natural ESD entry points: exposed conductive surfaces, direct routes into signal circuitry, cable shields, chassis interfaces and multiple reference domains. They also sit at the boundary between the product and an uncontrolled external environment.
An electrostatic discharge is not simply a high voltage applied to a pin. It is a fast transfer of charge, producing high current and broad spectral content. The resulting disturbance can enter through direct conduction, arc to nearby metalwork, couple capacitively into internal conductors or create a rapidly changing magnetic field around the discharge and return-current loop.
That distinction matters. Adding a suppressor to the visibly affected signal pin may do little if most of the current is flowing from the connector shell, across a poorly bonded panel and through the PCB reference plane before finding the chassis connection.
IEC 61000-4-2 defines a basic electrostatic discharge immunity test method. Product and product-family standards determine whether that method applies, the relevant test levels, performance criteria, discharge points and equipment configuration. Engineers should check the latest active editions rather than treating one familiar laboratory setup as universally applicable.
The discharge path decides what fails
Current follows impedance, not the line drawn as ground on the schematic. At ESD edge rates, a long trace, narrow neck, via chain or bonding strap can present enough inductive impedance to develop a damaging local voltage. Even a conductor with negligible DC resistance may perform badly during the initial transient.
A useful first question is therefore not, “Which component is sensitive?” It is, “Where does the discharge current enter, and where can it return?” Trace the physical loop through the connector, enclosure, PCB, cable shields, protective devices, mounting hardware and the test setup.
Connector shell current entering the PCB
A shielded connector normally needs a low-inductance route from its shell to the intended chassis or enclosure reference. If the shell is connected through a thin PCB trace or a long pigtail, the resulting impedance can force transient current into circuit 0 V. The microcontroller then sees ground movement, interface transceivers experience excessive common-mode voltage, and reset lines may cross their thresholds.
A short bond is not automatically a good bond. Its width, contact area, plating, mounting method and continuity around the connector aperture all affect high-frequency behaviour. Paint, anodising, loose hardware and insulating washers can turn apparently solid metalwork into a poor transient connection.
Signal-pin current bypassing the protection device
Protection components only work when the layout lets them intercept current. A transient voltage suppressor positioned away from the connector leaves a length of exposed trace that can capacitively or inductively couple into adjacent circuitry. The current may also pass a branch point before reaching the suppressor, dividing into the protected circuit.
Place the protective element close to the entry point, with a short and wide return to the appropriate reference. The choice of reference is part of the design. Dumping ESD current into digital 0 V can protect the interface pin while disturbing every circuit sharing that plane.
Device selection requires more than comparing stand-off and headline clamping voltages. Junction capacitance can compromise high-speed links, leakage may matter on high-impedance inputs, and dynamic resistance affects the residual voltage as current rises. Package and connection inductance add further overshoot. Manufacturer pulse plots and application data are useful, but their fixture and waveform conditions must be understood before extrapolating them to the assembled product.
Cable coupling creates a second entry route
A discharge to a connector shell or nearby enclosure can induce common-mode current on an attached cable. That cable may carry the disturbance to another port, an external power supply or connected support equipment. Removing the cable might make the symptom disappear, but that does not prove the connector itself is adequately protected. It changes the current path and the EUT configuration.
Cable type, shield termination, length, routing and connected peripherals must therefore be recorded. Otherwise, a passing retest may simply reflect a different coupling geometry.
Reset, corruption and latch-up point to different mechanisms
Not every ESD connector failure has the same root cause. The observed response provides useful diagnostic information.
- A clean, repeatable reset may indicate disturbance of reset, power supervision, clocking or firmware watchdog behaviour.
- Temporary communication loss can result from transceiver upset, common-mode disturbance or protocol recovery that has not been implemented robustly.
- Corrupted data suggests that the disturbance reached memory, a bus, an interrupt input or an inadequately filtered control line.
- A sustained high supply current can indicate semiconductor latch-up. Continued powering may cause thermal damage.
- A fault that clears only after removal of all power sources may involve latch-up, retained state or back-powering through an interface.
Instrument the product carefully. Monitor supply rails, reset, interrupt lines and relevant communications using probes and connection methods that do not create a new antenna or discharge route. Long oscilloscope ground leads can display ringing that belongs to the probe loop rather than the circuit. They can also alter the transient path enough to change the result.
Typical scenario
Consider an illustrative product with a metal-panel USB or Ethernet connector, a plastic rear enclosure and a PCB connected to the panel by mounting pillars. Contact discharge to the connector shell causes an immediate reset, while discharge to other accessible metalwork has no visible effect.
The tempting response is to replace the interface suppressor. A better investigation starts with the shell bond. If connector-shell current reaches chassis through a narrow PCB region and then a single mounting point, local circuit 0 V can rise relative to the rest of the assembly. The interface device, processor and reset supervisor may all remain within their individual pin ratings while the system still resets.
The team should reproduce the specified operating mode, map the discharge points and polarities, and record whether the fault follows shell discharge, accessible pin discharge where required by the applicable test plan, or indirect coupling. Temporary engineering modifications can then separate possible mechanisms. Examples include improving the shell-to-panel bond, changing shield termination, shortening a protection return or isolating a reset-line coupling route.
Make one controlled change at a time. Applying copper tape, ferrites and extra capacitors simultaneously may produce a pass, but it leaves no defensible explanation of what fixed the problem or whether the modification is suitable for production.
Early investigation using a suitable ESD generator and the correct ESD test accessories can reduce redesign risk before tooling and PCB layout are frozen. EMC Hire can support equipment selection, pre-compliance work, on-site testing and access to a test facility. Formal compliance testing can then provide stronger evidence for the technical file, Declaration of Conformity and stakeholder review where the selected conformity route permits self-certification.
Building a repeatable troubleshooting test
Start from the applicable product standard and test plan, not from the maximum setting on the simulator. Confirm the required discharge method, levels, polarities, points, number or rate of applications, EUT configuration and performance criteria. IEC 61000-4-2 is the basic immunity method, while the product standard or contractual specification supplies the product context.
Record enough detail for another engineer to reconstruct the test:
- EUT hardware and firmware revisions, operating mode and monitored functions
- connector population, cable types, routing, shield termination and peripherals
- discharge point, polarity, method and applied level
- ground reference plane, coupling-plane and simulator return-cable arrangement
- failure symptom, recovery method and supply-current behaviour
- temporary modifications, including their exact physical position
Photographs are often more useful than a paragraph describing cable placement. A moved return cable or cable harness can change the loop area and coupling, producing a different result even when the simulator setting is unchanged.
Test equipment should be suitable for the required method and supported by valid calibration. EMC Hire uses test equipment with calibration traceable through an appropriate ISO/IEC 17025 accredited calibration provider. That traceability supports measurement confidence, repeatability and comparison between development and formal testing. It does not make a physical instrument, or the test facility using it, “ISO 17025 accredited”.
When to Hire EMC Equipment
ESD generators are often needed intensively for a few days during prototype debugging, then not again until the next hardware revision. Hiring can avoid capital expenditure on equipment that spends most of its life in storage while still requiring servicing, verification, accessories and calibration management.
Rental also lets a team select equipment for the defined test window rather than buying around one programme and discovering that a later product needs different capability or accessories. It is particularly useful when several projects converge, a laboratory booking is still weeks away, or engineers need the generator beside the design bench to narrow a fault quickly.
The test environment still matters. Informal bench testing can locate vulnerable paths, but it should not be misrepresented as formal evidence if the specified setup has not been reproduced. Where controlled facilities or engineering support are needed, booking pre-compliance or formal compliance testing may be more efficient than attempting to recreate the full arrangement in-house.
EMC Hire can help determine whether equipment hire, an on-site investigation or a facility booking is the more proportionate approach. Related disturbances may also justify separate conducted immunity testing, but conducted RF immunity is a different phenomenon and test method from ESD.
Common EMC Testing Mistakes to Avoid
Discharging every connector pin without checking applicability
Applying a discharge to arbitrary pins can damage interfaces in a way the applicable standard never intended. Identify accessible conductive parts, contact-discharge points and air-discharge points from the current product requirements and documented test plan.
Moving the simulator return cable between tests
The return-cable position affects coupling and current-loop geometry. Uncontrolled placement weakens repeatability and can turn an apparent design improvement into a setup artefact.
Changing cable routing after a failure
Cables are part of the coupling structure. Moving one away from the enclosure can remove a failure without correcting the product. Mark positions and photograph the arrangement before modifications begin.
Fitting protection without examining its return
A suppressor with a long return connection may develop substantial transient voltage across that connection. The schematic then looks protected while the PCB layout leaves the interface exposed.
Testing an unrepresentative operating mode
An idle interface may pass while active traffic, a connected charger or a high-current processor state fails. Testing only the easiest mode creates false confidence and an incomplete evidence trail.
Recording only pass or fail
Without polarity, discharge point, level, configuration and recovery details, the result cannot be reproduced or used effectively for root-cause analysis. A short video of the symptom can supplement, but not replace, structured test records.
Frequently Asked Questions (FAQs)
Why does negative polarity fail when positive polarity passes?
The current direction changes junction biasing, suppressor behaviour and local reference movement. Semiconductor structures may therefore respond asymmetrically. Treat polarity sensitivity as diagnostic evidence, not proof that the simulator is inconsistent.
Should the connector shield connect to chassis or circuit 0 V?
There is no universal answer, but directing shield current into circuit 0 V often increases internal disturbance. The decision depends on enclosure construction, isolation, safety requirements, cable shielding and system architecture. The connection must be assessed as a high-frequency current path, not only for DC continuity.
Can adding capacitance to reset solve the problem?
It may suppress a narrow reset pulse, but excessive capacitance can violate supervisor timing, delay start-up or mask disturbance elsewhere. First establish whether reset is being asserted legitimately, coupled directly or triggered by a supply dip.
How can latch-up be distinguished from firmware lock-up?
Monitor supply current and recovery behaviour. Abnormally high current that persists until power removal is consistent with latch-up, although further investigation is needed. Firmware lock-up may leave current near normal and might recover through watchdog or reset action.
Does a successful pre-compliance test prove conformity?
No. Pre-compliance testing improves confidence and can generate calibrated engineering data, but conformity depends on the applicable legislation, product standards, configuration, documentation and assessment route. The manufacturer or responsible economic operator remains responsible for confirming those requirements.
When should formal testing replace bench debugging?
Move to a controlled test programme once the design is stable enough to justify representative testing, or earlier if setup uncertainty is blocking diagnosis. Formal testing can strengthen the compliance evidence trail, while some defence, automotive or aerospace programmes may require final testing by an appropriately accredited laboratory under contractual or programme rules.
Plan the next investigation
For a deeper discussion of the method, see EMC Hire’s EN 61000-4-2 ESD testing guidance. Always verify the latest active standard edition, product-specific requirements, levels, configurations, methods, performance criteria and documentation obligations before fixing the test plan.
If an ESD connector failure is delaying a design release, the EMC Hire engineering team can help review the likely discharge path, specify suitable hire equipment or arrange pre-compliance, formal compliance or on-site testing. Test facility space can also be booked for controlled investigation. Call +44 (0)1462 817111 or email sales@emchire.co.uk with the product type, applicable standard, connector details and observed failure mode.
Disclaimer: Content is for informational purposes only and does not constitute formal engineering or regulatory advice. Always verify testing procedures against current official standards (e.g., ISO, MIL-STD, DEF STAN). EMC Hire Limited accepts no liability for outcomes resulting from the use of this information.